
- Ppk ≥ 1.67 initial key, ≥ 1.33 general; example Ppk ≥ 1.67 at the initial study on key characteristics.
- Hexagon GLOBAL S CMMs, vision machines, laser microscope, SURFCOM 1800D.
- XRF verifies every incoming lot against its mill certificate.
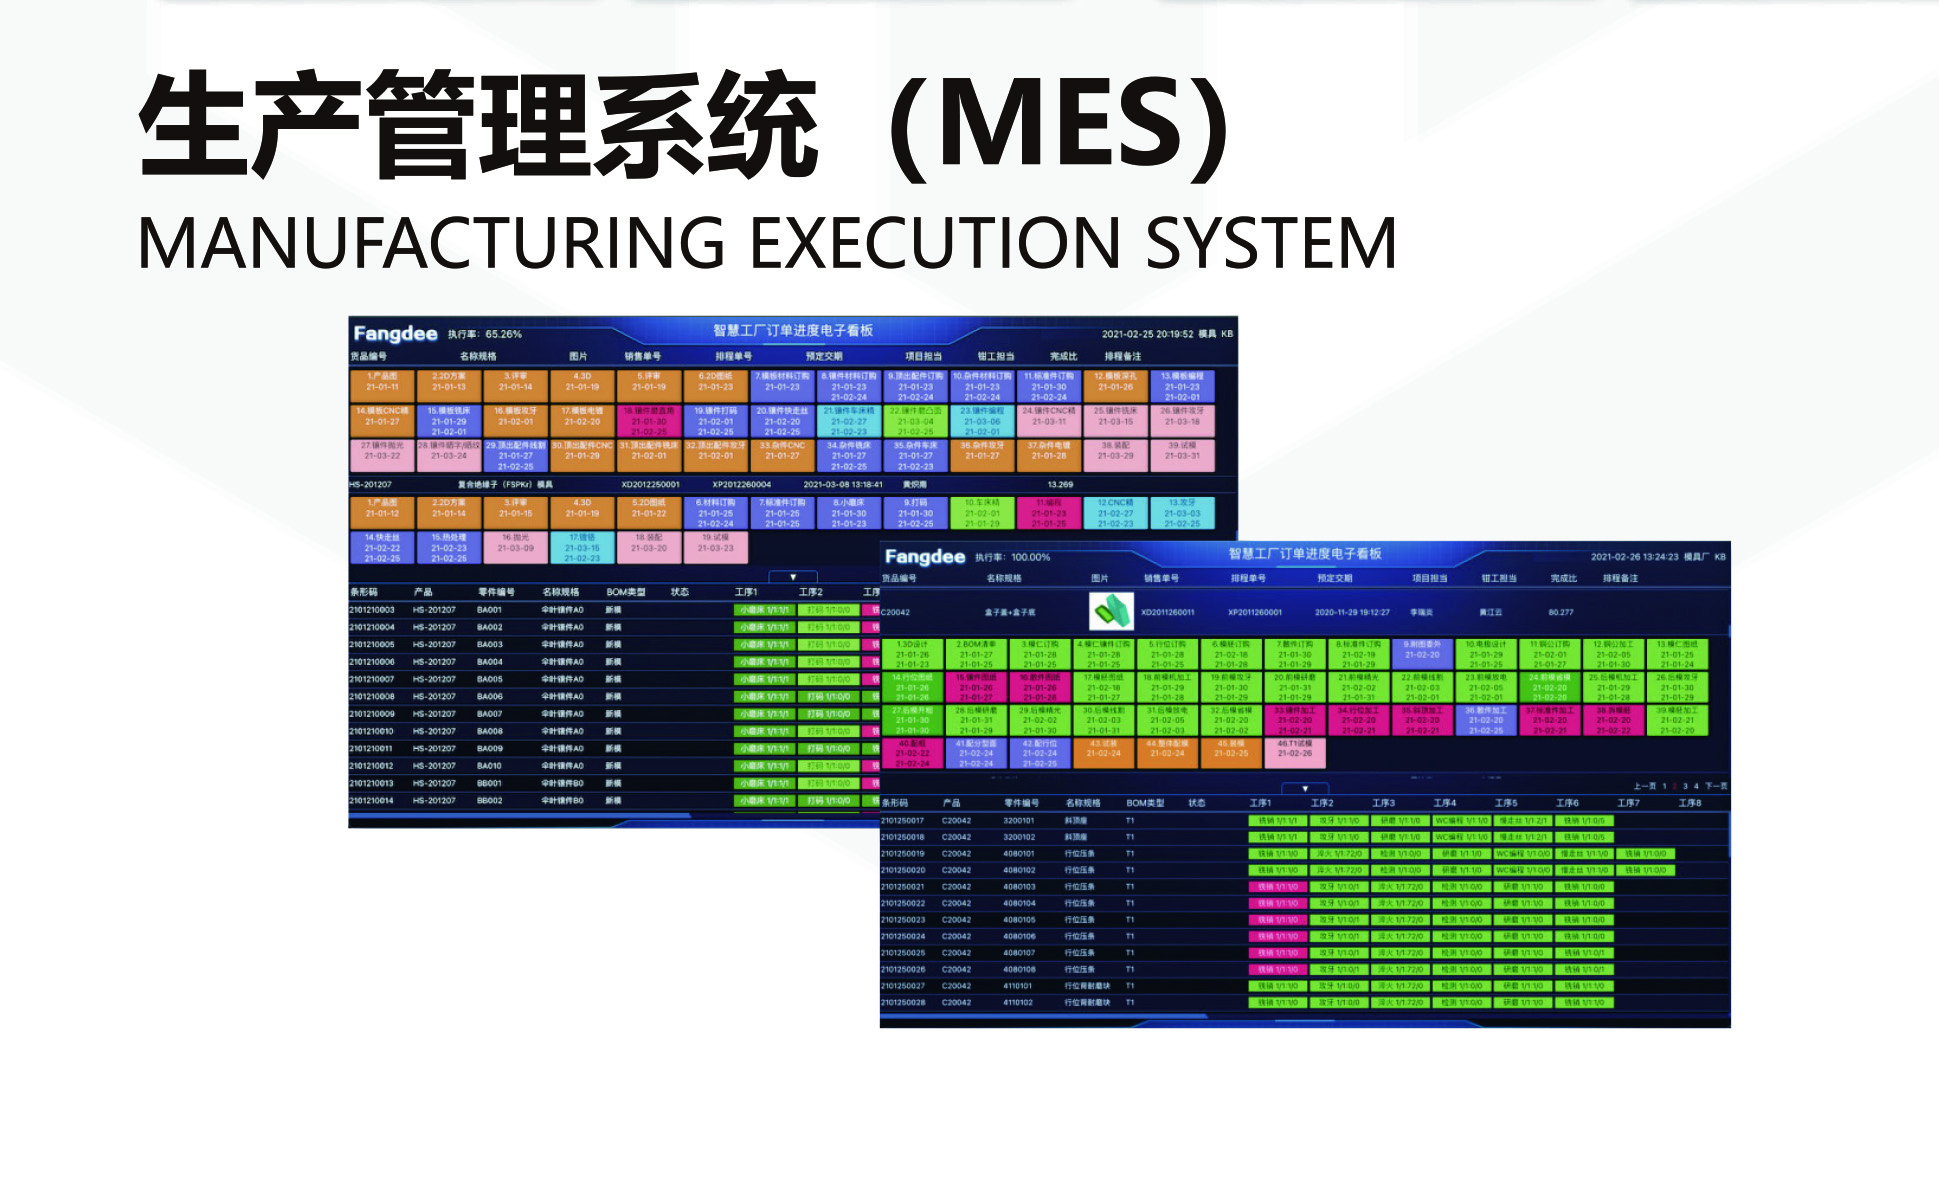
- ISO 9001 + IATF 16949 + ISO 14001 — certificates behind a trusted schedule.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
Why is quality the thing that keeps a lead time on schedule?
Because rework is the hidden lead time. A part that fails inspection must be re-made, re-measured, and re-shipped — every step doubling the schedule. Quality control prevents that by producing good parts on the first pass, which is why the fastest supplier and the most capable supplier are usually the same one.
How does Cpk predict an on-time part?

Cpk tells you whether a process holds tolerance consistently or drifts into rework. A key-characteristic target of Ppk ≥ 1.67 initial means first-pass parts, not sorted rejects. Here, the SPC record shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) on a representative length characteristic (76.1–76.5 mm), with general characteristics held to Cpk ≥ 1.33 — the statistical reason the schedule holds.
How does measured inspection prevent a schedule slip?
Inspection catches a drift before it becomes a scrapped batch. The Hexagon GLOBAL S CMMs check critical dimensions, with vision machines, a gear measuring center, a KEYENCE VK-X3000 laser microscope, and a SURFCOM 1800D for finish. A measured value on every critical dimension means a problem is caught at the machine, not at your receiving dock — where it would restart the clock.
How does material control avoid a delayed re-order?
The wrong alloy is the failure that forces a full re-order — the longest lead time of all. Every incoming lot here is XRF-checked against its mill certificate, so a substituted grade is stopped at the door before it can produce a part that passes every dimensional check and still fails. That control removes the most expensive schedule slip in the book.
Which certificates back the quality system?
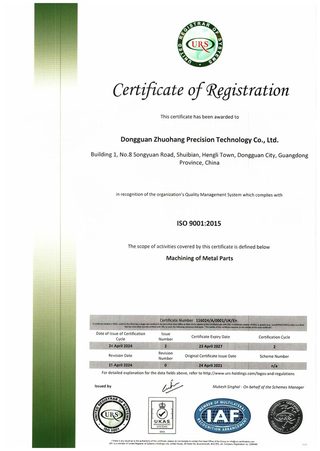
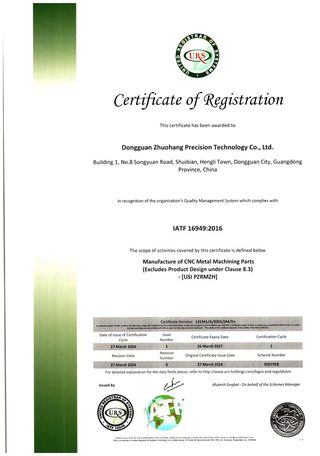
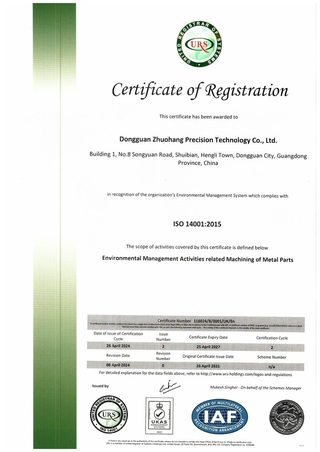
Three certificates, with numbers you can verify and scope stated honestly:
| Standard | Certificate number | Scope |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Honest scope note: IATF 16949 excludes product design under Clause 8.3 — a build-to-print manufacturer. A supplier that states its scope honestly is also the one whose schedule you can trust, because over-promising anywhere usually means over-promising everywhere.
How does traceability avoid a schedule-wide stop?
When a non-conformance surfaces, traceability lets you contain it to one lot instead of stopping every order. The MES/ERP system here records raw material source, process parameters, machine data, batch, operator, and inspection results on every lot, so a problem is isolated and fixed, not allowed to spread into a schedule-wide halt.
What quality evidence proves the schedule is real?
Ask for the evidence that a fast lead time is not a fast disaster: a CMM report with measured values, an SPC chart with the Cpk stated, and a material certificate. A supplier that ships these with the parts is showing you why the date holds — first-pass parts, not promises.
How do inspection stages catch a problem early?
Every inspection stage exists to catch a failure one step earlier, because a problem caught at the machine costs minutes and one caught at your dock costs a reschedule. The stages line up like this:
| Stage | What it catches | Schedule effect if missed |
|---|---|---|
| Incoming material XRF | Substituted alloy vs mill certificate | A full re-order — the longest delay |
| In-process measurement | Tool wear drifting a dimension | A scrapped batch re-run |
| CMM verification | Critical dimensions out of tolerance | Rework or re-make before ship |
| Final inspection | Surface finish and profile | A returned shipment and a restart |
your question is not "do you inspect" — every supplier says yes — but "at which stage do you catch the failure, and what does that cost the schedule." Earlier is always cheaper and faster.
What should you ask a quality manager before you commit?
Five questions tell you whether the quality system is real or rehearsed. Ask them directly.
- Show me the SPC chart for my characteristic — a Cpk number without a chart is a claim; Ppk ≥ 1.67 at the initial study on key characteristics with a chart is a process.
- What does your key-characteristic target actually require? The answer should be Ppk ≥ 1.67 initial for key characteristics and Cpk ≥ 1.33 for general — stated, not waved at.
- How do you verify the alloy before the first cut? The honest answer is an XRF check against the mill certificate, on every lot.
- Where is your IATF 16949 scope drawn? A build-to-print shop that excludes product design under Clause 8.3 is telling you the truth; one that does not is worth a harder look.
- What evidence ships with the parts? A CMM report, an SPC chart, and a material certificate are the proof the date holds.
How does first-pass yield become the schedule itself?
First-pass yield is the quiet number behind every on-time shipment. A part that passes on the first pass ships once; a part that fails and is reworked ships twice — the second time through the same schedule. When first-pass yield is high, the schedule holds because nothing re-enters it. When it is low, the schedule quietly absorbs rework that the quote never showed.
Yield is a product of the same controls the rest of this page describes: a centered process, verified material, calibrated measurement, and an in-process check that catches drift before it becomes scrap. Put those together and most parts pass the first time, which is why Ppk ≥ 1.67 at the initial study on key characteristics is not a bragging number but a schedule number — it is the statistical reason the fastest supplier and the most capable supplier are the same one.
your lens is simple: a supplier that talks about first-pass yield is talking about your delivery date. A supplier that only talks about final inspection is telling you how it finds late parts, not how it avoids them.
How does in-process measurement differ from final inspection?
Final inspection catches a bad part after it is made; in-process measurement catches a drifting process before it makes one. The difference is the whole schedule, because a part caught at the machine costs minutes and a part caught at your dock costs a reorder and a reset launch.
In-process measurement watches the process, not just the part. A tool wears, a dimension drifts, and the operator sees the trend in the measurement before the part falls out of tolerance. The Hexagon GLOBAL S CMMs, vision machines, a KEYENCE VK-X3000 laser microscope, and a SURFCOM 1800D sit on the floor for exactly this, so a drift is caught at the machine, corrected, and the schedule continues instead of restarting.
your question is the one that separates the two: at which stage do you catch the failure, and what does that cost the schedule? The answer you want is "in-process, at the machine", because earlier is always cheaper and faster.
How does tool wear show up in a quality system?
Tool wear is the most common source of dimensional drift in machining, and a quality system has to see it coming. As a cutter wears, it cuts slightly smaller or slightly larger, and the drift shows up in the measurement trend long before the part leaves tolerance. A shop that monitors that trend changes the tool before the scrap; a shop that does not changes the tool after the scrap.
Tool-life management is the discipline behind it. A set tool life, a replacement schedule, and an in-process check at the tool-change point keep the process centered. That is how a ±0.003 mm (milling) / ±0.002 mm (turning) process stays a ±0.003 mm (milling) / ±0.002 mm (turning) process across a thousand parts instead of drifting into rework halfway through the run.
The schedule link is direct: unmanaged tool wear is the difference between a batch that ships and a batch that is re-run. A quality system that names its tool-life policy is one that has thought about your delivery date; a system that cannot is one that will discover tool wear the hard way, on your order.
How does a calibration program keep the schedule honest?
A measurement is only as good as the instrument behind it, and an instrument drifts too. A CMM or a profilometer that has not been calibrated reports numbers you cannot trust, and a trusted number is the difference between shipping and re-measuring. Calibration is the part of the quality system that keeps the schedule honest at the point where a part is accepted or rejected.
The calibration program covers the instruments this page names: the Hexagon GLOBAL S CMMs, the vision machines, the laser microscope, the SURFCOM 1800D. Each is checked on a schedule and against a traceable standard, so a measured value on a critical dimension means the dimension, not the instrument's error. A supplier that can show calibration records is one whose acceptance decision you can plan a launch around.
your check is one line: when was the last calibration, and can I see the record? A supplier that produces the record without hesitation is a supplier whose CMM reports mean something.
How does a CAPA loop prevent the next schedule slip?
A corrective-and-preventive-action loop is what turns one mistake into zero repeats, and that is a schedule asset. When a non-conformance is found — a drift, a wrong alloy, a missed tolerance — the loop asks why it happened and what changes so it cannot happen again. The alternative is to fix the part and wait for the same problem on the next order.
The loop matters to your lead time because a recurring problem is a recurring delay. A supplier that fixes the root cause of a rework removes that rework from every future order; a supplier that only re-makes the part will re-make it again on yours. The CAPA loop is how a plant gets faster over time instead of staying the same speed with better excuses.
Ask what the last corrective action was and what changed because of it. The specificity of the answer tells you whether the plant learns from its schedule slips or just survives them.
How do you read an SPC chart for what it really tells you?
An SPC chart is a picture of whether a process is under control or just lucky, and reading it is a skill worth having. The chart plots a measured characteristic over time, against the tolerance limits and the control limits. Points inside the control limits, spread evenly around the center, mean the process is stable. Points drifting toward a limit mean a tool is wearing or a setup is shifting — a rework coming.
The number to pull from the chart is Cpk, and the targets are Ppk ≥ 1.67 initial for key characteristics and Cpk ≥ 1.33 for general. Here the record shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) on a representative length characteristic of 76.1–76.5 mm — held by capability, not by sorting. The difference matters: a capable process ships first-pass parts; a sorted process ships the good ones and hides the bad ones, and the hiding is what reaches your dock.
A chart with Cpk stated is a process under control. A number without a chart is a claim. Ask for the chart, and you will know which one you are looking at.
What this shop actually runs
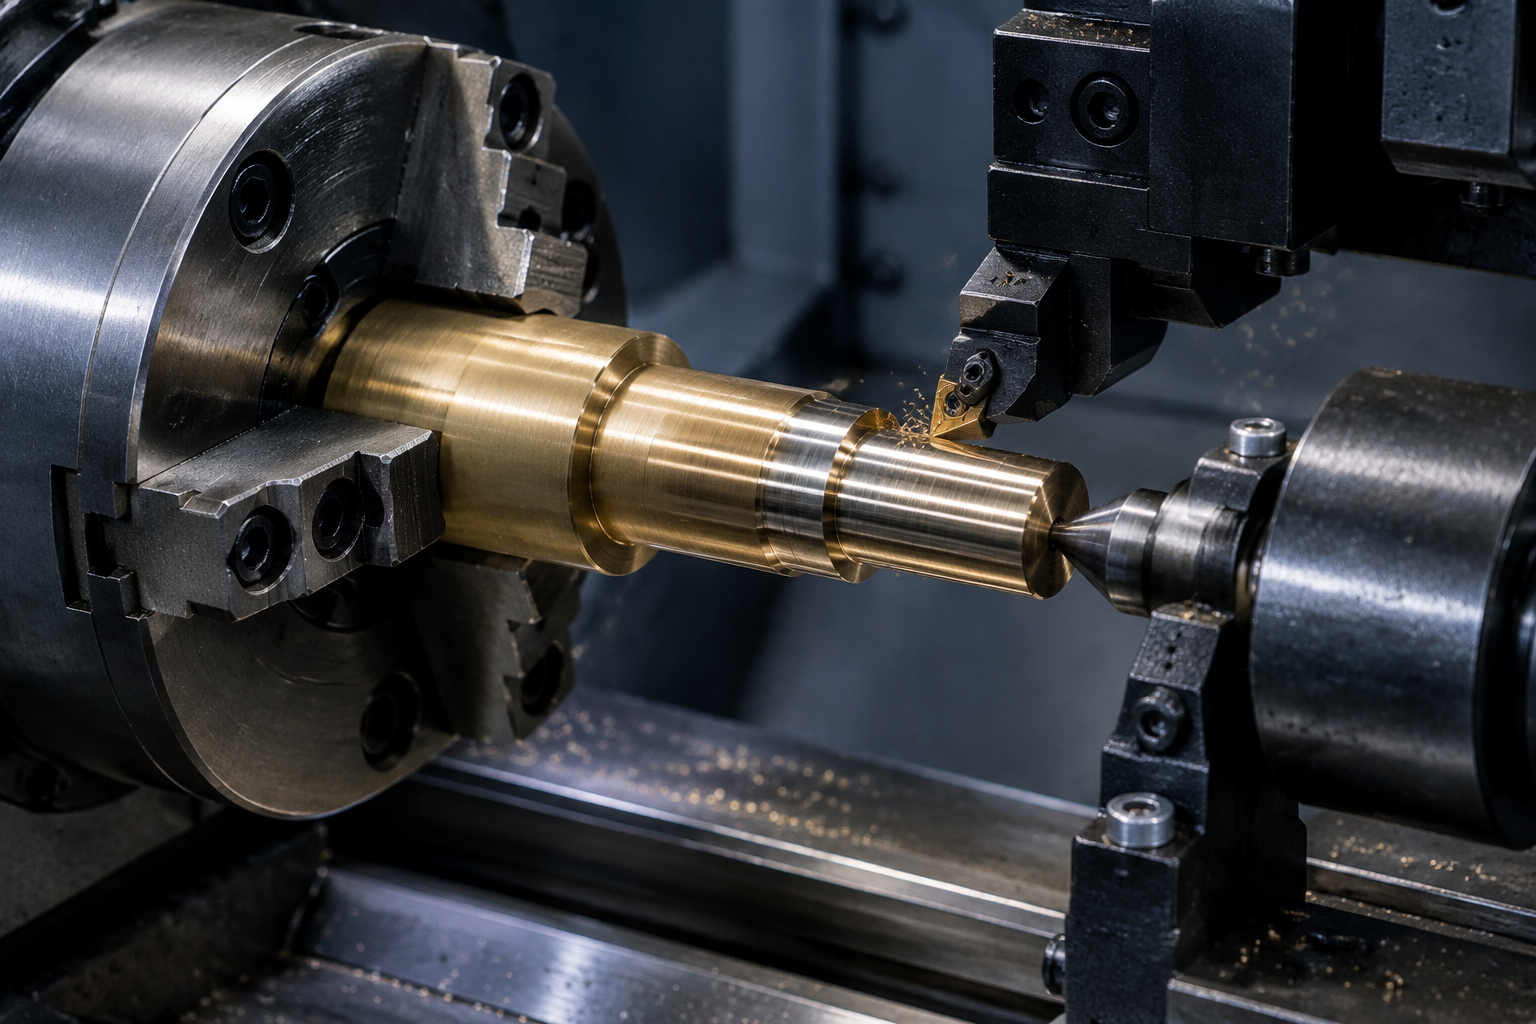

If you ask for capability evidence, you deserve a specific answer. This facility operates 100+ CNC machines across 6,800 m2 in Dongguan, China, staffed by 100+ people. The machines, listed by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Matched to compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Matched to prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Matched to long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Matched to shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Matched to hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands: ±0.003 mm milled, ±0.002 mm turned, ±0.002 mm ground or wire-cut. Capability indices: Ppk >= 1.67 at the initial study; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En) · IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded) · ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, since 2005).
Service area: we supply Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide delivery from China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ready to machine your parts?
Send your drawing to [email protected] or call +86 13126536955 for a quote.
Frequently Asked Questions
Why does quality keep a lead time on schedule?
Rework is the hidden lead time — a part that fails inspection must be re-made and re-shipped, doubling the schedule. Quality control produces good parts on the first pass, which is why the fastest supplier is usually the most capable one.
What process capability should a factory prove?
In short, Key characteristics should be held to Ppk ≥ 1.67 initial and general characteristics to Cpk ≥ 1.33. On a representative length characteristic of 76.1–76.5 mm, the SPC record here shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) — held by capability, not by sorting.
How are dimensions verified?
Critical dimensions are checked on Hexagon GLOBAL S CMMs, with vision measuring machines, a KEYENCE laser microscope, and a SURFCOM 1800D for surface finish and profile, so every critical dimension ships with a measured value.
What certificates does the factory hold?
In short, ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En), under Dongguan Zhuohang Ltd; IATF 16949 excludes design under Clause 8.3, a build-to-print manufacturer stated honestly.
How is incoming material verified?
Every incoming lot is XRF-checked against its mill certificate, so a substituted alloy is stopped at the door before it can produce a part that passes every dimensional check and still fails — avoiding a full re-order.
Rapid Prototyping China Quality — Related Pages
Continue reading: Rapid Prototyping China · Rapid Prototyping China Factory · Rapid Prototyping China Services
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- ASTM E8/E8M-21 — Standard Test Methods for Tension Testing of Metallic Materials