
Rapid Prototyping China Services
Mill-turn removes the handoff between a lathe and a mill, which is a step, a queue, and a chance for schedule slip — all in one. On Mazak and Brother class centers holding ±0.003 mm (milling) / ±0.002 mm (turning), a part with turned and milled features is done in one clamping, which shortens the lead time by removing a whole operation from the critical path.
How does grinding fit the schedule?
Grinding is a finishing pass, and it belongs on the schedule only where the function demands it — a bearing seat or press-fit diameter at ±0.002 mm. Adding grinding where turning already meets the print wastes lead time for no gain. The planning discipline is to schedule the grind only where the print requires it.
How does one roof shorten the total schedule?
When milling, turning, mill-turn, and grinding run on one 6,800 m² floor, the part moves between machines, not between vendors — no transit time, no third-party queue, no handoff delay. The total schedule is the sum of the operations, not the sum of the operations plus a supply chain of waiting.
How do you validate the schedule with one part?
Order one part at the MOQ of 1 piece and watch the actual lead time against the quoted tier. That single part validates the schedule and the process together, so when you release volume, the lead time you were promised is the lead time you already measured.
How do you match the service to the geometry?
The geometry decides the service, and the service decides the setup count, so matching them is a lead-time decision made before the first cut. The rule of thumb lines up like this:
| Geometry | Service | Setup count and schedule effect |
|---|---|---|
| Round part, turned features only | Turning | One setup, the fastest tier |
| Prismatic part, several faces | 3-, 4-, or 5-axis milling | More setups, longer than turning |
| Turned plus milled features | Mill-turn | One clamping — removes a lathe-to-mill handoff |
| Bearing seat or press-fit diameter | Grinding | Finish pass at ±0.002 mm |
A wrong match is a hidden queue: a part that could turn in one setup gets routed through milling setups it does not need, and the schedule pays for it. Ask the service to justify the routing against your geometry, not just to list the machines it owns.
What should you ask a machining service before you send a drawing?
Five questions expose whether a service plans its routing or just quotes a number. Ask them before you send the file.
- Which service — and how many setups — does my part need? A real answer names the process and the setup count.
- Where does the part move between operations? The answer you want is between machines on one floor, not between vendors.
- What tolerance does each service hold, and where does my print force the tighter process? Grinding should appear only where the print requires ±0.002 mm.
- How does a spike in one process affect my job? Per-process parallel capacity is the difference between routing and queuing.
- How do I validate the schedule before volume? One part at the MOQ of 1 piece, measured against the quoted tier, is the honest test.
How do axis counts change the setup math?
Axis count is a setup-count decision, and setups are the schedule. A 3-axis mill reaches one face per setup; a 4-axis reaches faces around a rotary axis; a 5-axis reaches five sides of a cube in one clamping. The more faces a machine reaches without re-clamping, the fewer handoffs the part carries, and every handoff removed is queue time removed.
| Machine | Reach per setup | Schedule effect |
|---|---|---|
| 3-axis mill | One face | Multiple setups on multi-face parts |
| 4-axis mill | Faces around one rotary axis | Fewer setups than 3-axis |
| 5-axis mill | Five sides in one clamping | Complex geometry in fewer setups |
| Mill-turn | Turned plus milled in one clamping | Removes the lathe-to-mill handoff |
The rule is simple: match the axis count to the geometry. Routing a five-sided housing through a 3-axis machine to save an hourly rate is a false economy — the setups you add cost more in queue time and locating error than the machine saves. The hourly rate is the small number; the schedule is the big one.
How do you choose between turning, milling, and mill-turn?
The choice is made by the part's dominant feature, not by preference. A part that is mostly round — a shaft, a pin, a bushing — belongs on a lathe, where it is done in one setup. A part that is mostly prismatic — a housing, a bracket, a plate — belongs on a mill. A part that mixes turned and milled features belongs on a mill-turn, where both happen in one clamping.
The cost of a wrong choice is hidden queue time. A round part routed through milling setups it does not need carries extra handoffs for no reason; a prismatic part pushed onto a lathe the wrong way does not fit at all. The service choice is the first lead-time decision, and it should be made by reading the geometry, not by reading the machine list.
When the part mixes features, mill-turn is usually the schedule answer. It removes the handoff between a lathe and a mill — a step, a queue, and a locating error all gone at once — and on Mazak and Brother class centers it holds ±0.003 mm (milling) / ±0.002 mm (turning), so the tolerance does not force you back to two machines.
How does tooling affect a process's schedule?
Tooling is the part of the schedule that never appears on the quote. A part that needs a standard end mill starts fast; a part that needs a long-reach tool, a custom form tool, or a tiny-diameter cutter for a deep pocket starts slower, because the tool either waits on a toolroom or forces slower feeds to survive the cut.
Tooling shows up in three places: the programming step (selecting and proving the tool), the cutting step (the feed a tool can hold), and the finishing step (a dedicated finish tool for a tight surface). A supplier that owns the tooling library for your part starts sooner than one that has to order it. A supplier that talks about the tooling behind your part is thinking about the schedule, not just the machine.
your question is pointed: which tools does my part need, and are they on the shelf or on order? The answer tells you whether the first week of your lead time is cutting metal or waiting on a toolroom.
How do tolerances and surface finish differ across processes?
Each process holds a different tolerance band, and the band sets what the process can promise. Milling, turning, and mill-turn hold ±0.003 mm (milling) / ±0.002 mm (turning). Grinding holds ±0.002 mm. Surface finish follows the same ladder: milling and turning land around Ra 1.6 to 3.2 µm as-cut, while grinding reaches Ra 0.8 µm and finer.
| Process | Typical tolerance | Typical finish |
|---|---|---|
| Milling / turning / mill-turn | ±0.003 mm (milling) / ±0.002 mm (turning) | Ra 1.6–3.2 µm as-cut |
| Precision grinding | ±0.002 mm | Ra 0.8 µm and finer |
The planning discipline is to schedule the tighter process only where the print demands it. A bearing seat or press-fit diameter at ±0.002 mm justifies the grind; a general surface at ±0.002 mm does not. Adding grinding where turning already meets the print is a schedule cost with no functional return.
How does material machinability interact with each process?
Material machinability is not a single number — it interacts with the process. Aluminum turns and mills fast across the board. Stainless steel and alloy steel cut slower in every process and wear tools faster, but the penalty is heavier in milling, where the tool is interrupted and heat builds at the edge, than in turning, where the cut is continuous.
The practical effect is that the same material can move a part across a tier differently depending on the process. A 304 stainless part that is mostly turned stays in a faster tier than a 304 stainless part that is mostly milled, because the milling cut is where the material fights back hardest. The service choice and the material choice are made together, not one after the other.
The floor machines aluminum, stainless steel, carbon and alloy steel, brass, copper, titanium, magnesium, and engineering plastics — with every incoming lot XRF-checked against its mill certificate, so the grade that hits the machine is the grade on the drawing. The grade matters because machinability varies within a family: 6061-T6 cuts far more freely than 7075-T6, and 304 differs from 316 at the tool edge.
How do you audit a service routing before you commit?
The routing is the schedule, written down. Read it the way you would read a drawing, and ask the questions that expose whether it was engineered or invented:
- Which process, and how many setups, does my part need? The answer should name the process and the setup count, not a vague "we can do it."
- Where does the part move between operations? The answer you want is between machines on one floor, not between vendors.
- Which tolerance does each process hold, and where does my print force the tighter one? Grinding should appear only where ±0.002 mm is required.
- How does a spike in one process affect my job? Per-process parallel capacity is the difference between routing and queuing.
- Which tools does my part need, and are they in-house? An on-shelf tool starts now; an on-order tool starts later.
A service that can answer these in specifics is showing you a routing that will hold. A service that answers in adjectives is showing you a quote that will move.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
What this shop actually runs
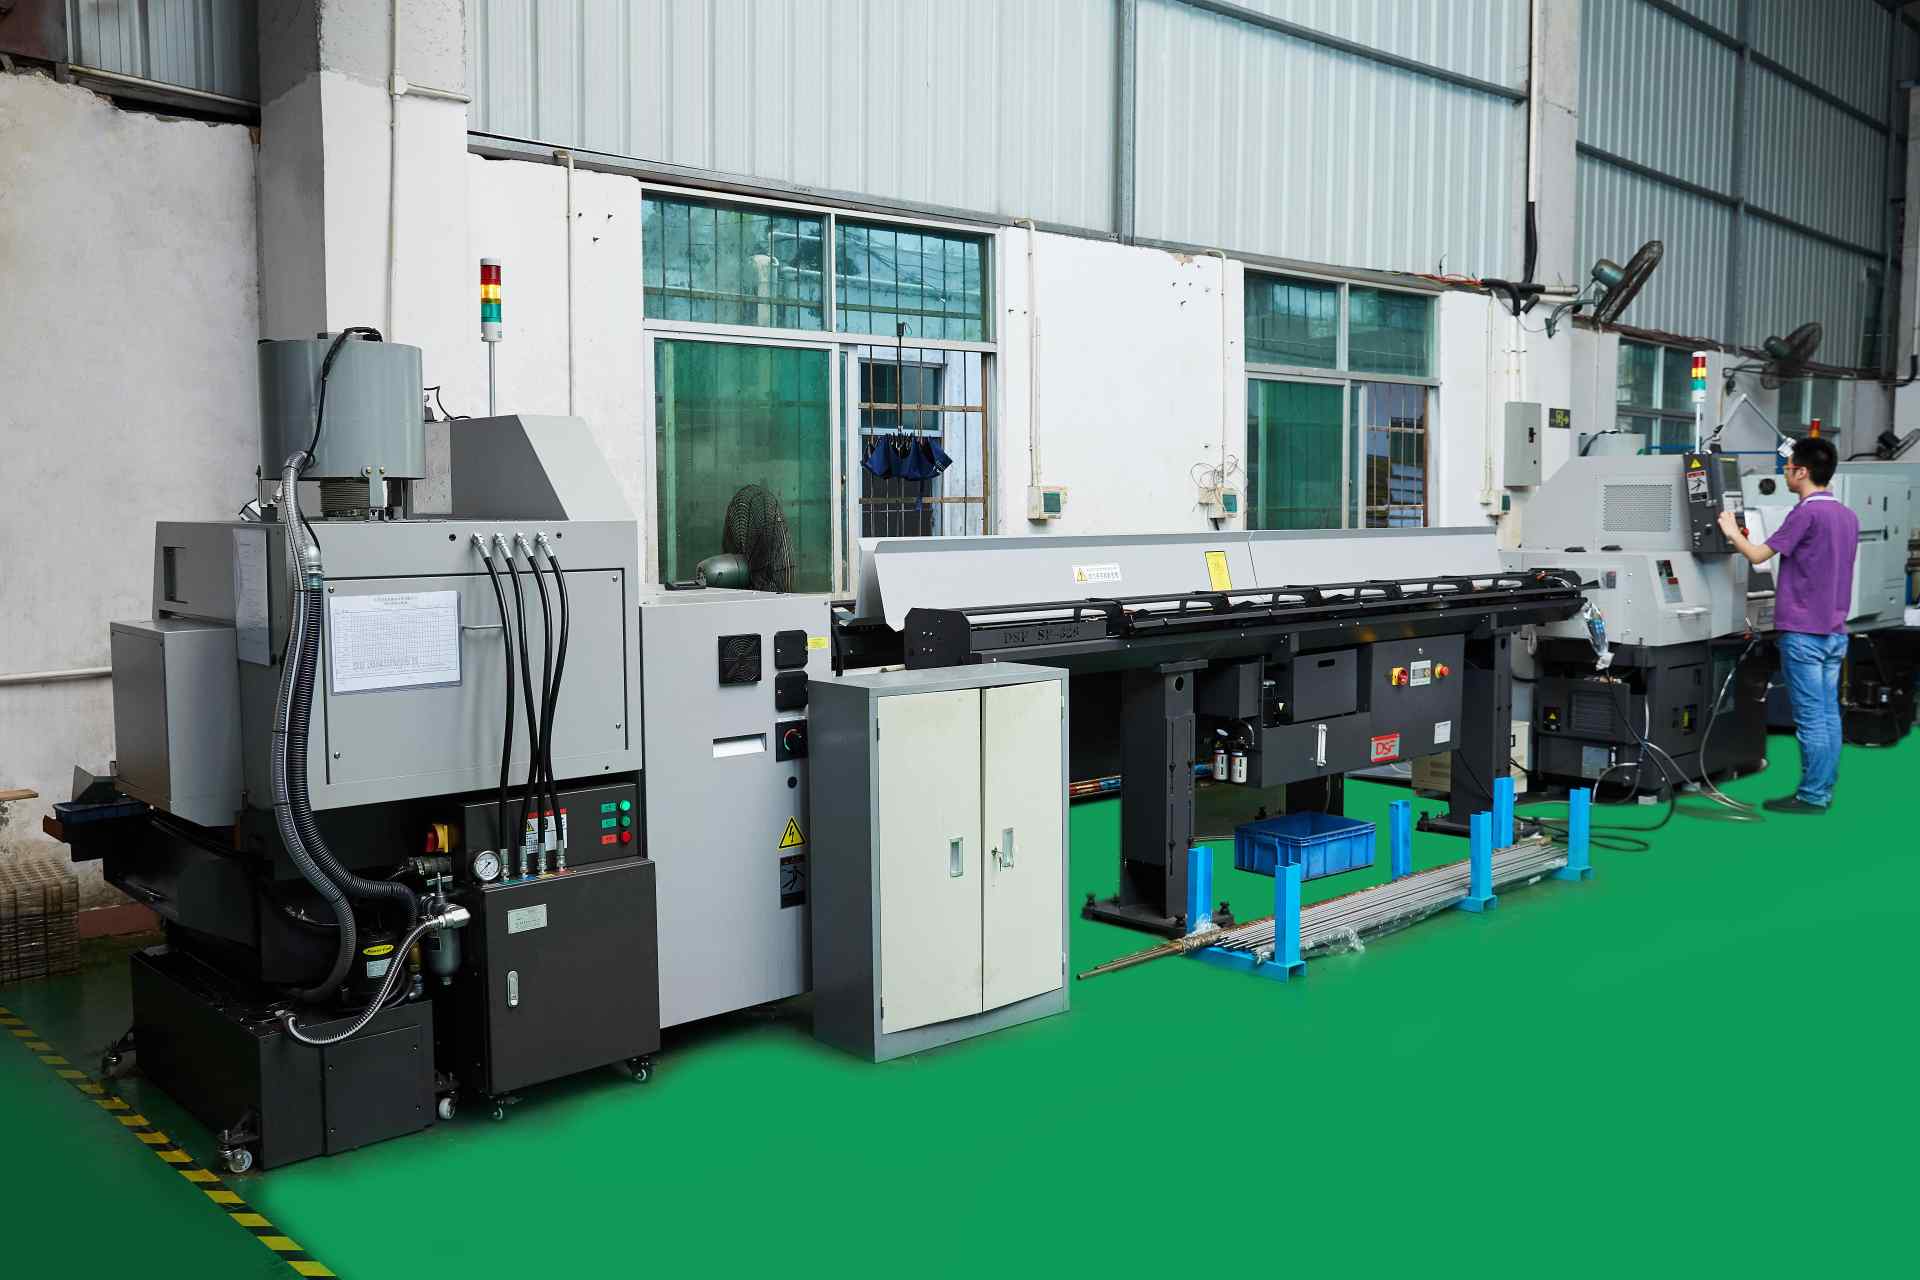
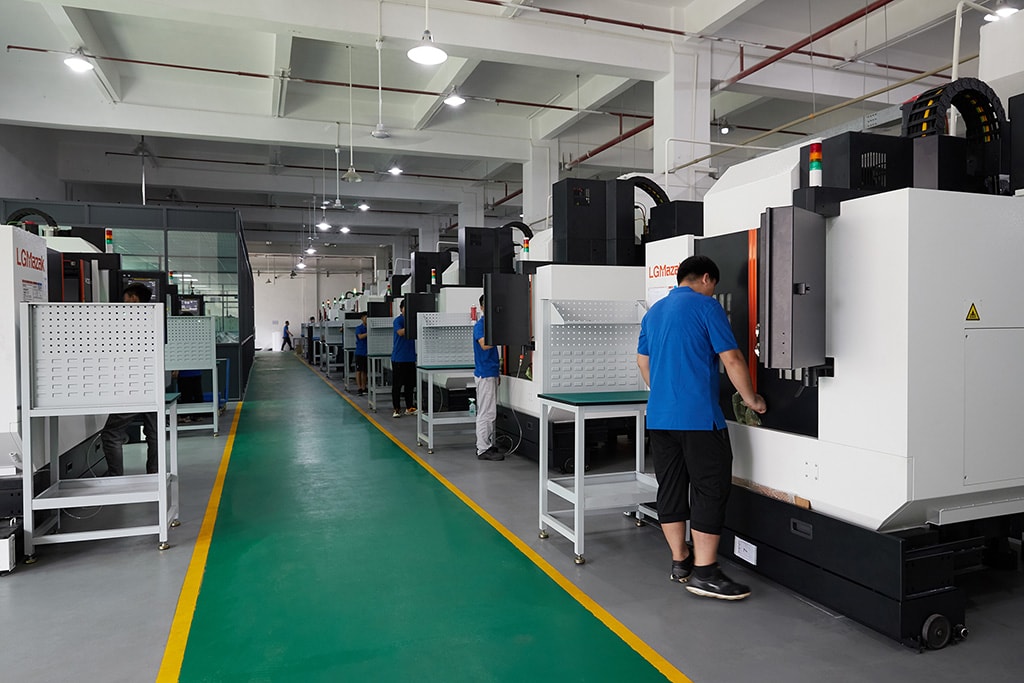
If you ask for capability evidence, you deserve a specific answer. This facility operates 100+ CNC machines across 6,800 m2 in Dongguan, China, staffed by 100+ people. The machines, listed by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Matched to compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Matched to prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Matched to long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Matched to shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Matched to hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands: ±0.003 mm milled, ±0.002 mm turned, ±0.002 mm ground or wire-cut. Capability indices: Ppk >= 1.67 at the initial study; Cpk >= 1.33 ongoing in production.
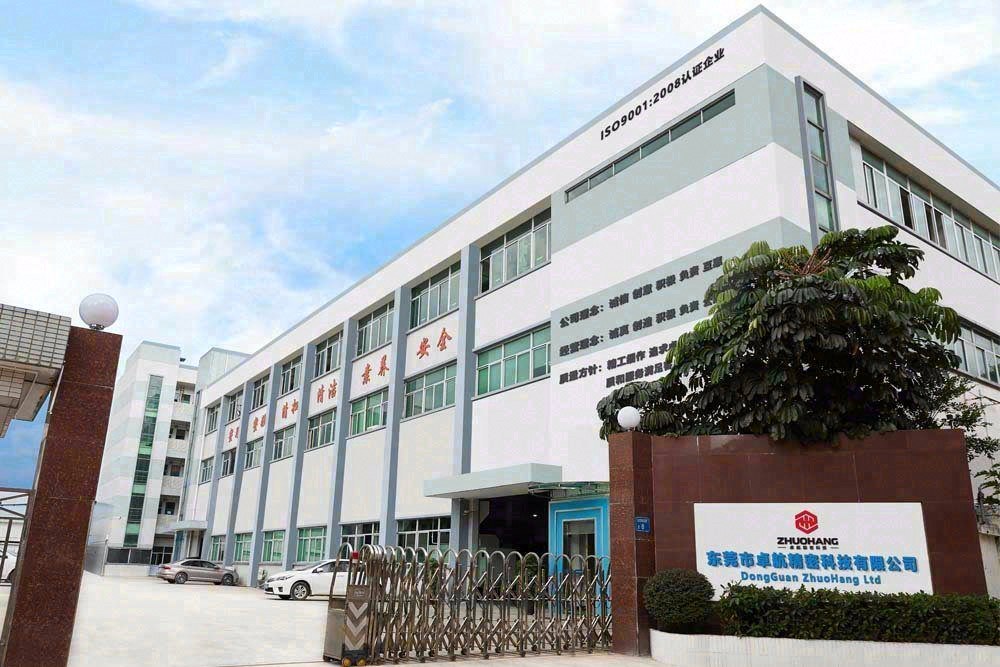
Certifications: ISO 9001:2015 (116024/A/0001/UK/En) · IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded) · ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, since 2005).
Service area: we supply Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide delivery from China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ready to machine your parts?
Send your drawing to [email protected] or call +86 13126536955 for a quote.
Frequently Asked Questions
How does the service choice affect lead time?
The service sets the number of steps and setups, which sets the lead time. Turning is one setup and fast; milling adds setups; mill-turn removes a handoff. Choosing the right service is the first lead-time decision you make.
What tolerances do your services hold?
In short, ±0.003 mm (milling) / ±0.002 mm (turning) for milling, turning, and mill-turn, and ±0.002 mm for precision grinding, verified on Hexagon CMMs. On a representative length characteristic, the SPC record shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) against an initial-study target of Ppk ≥ 1.67.
How does capacity speed up a prototype?
50+ three-axis, 20+ four-axis, and 20+ five-axis centers plus 25+ lathes mean a job routes to the first open machine that fits it, and each process has its own capacity, so a prototype does not queue behind unrelated work.
How does mill-turn shorten lead time?
Mill-turn does turned and milled features in one clamping, removing the handoff between a lathe and a mill — a step, a queue, and a schedule risk all eliminated at once.
Do the services run under one roof?
Yes — milling, turning, mill-turn, and grinding run on one 6,800 m² floor, so the part moves between machines rather than vendors, with no transit time or third-party queue in the schedule.
How do I validate the schedule before volume?
Order one part at the MOQ of 1 piece and measure the actual lead time against the quoted tier. That single part validates the schedule and the process together before you release volume.
Continue reading: Rapid Prototyping China · Rapid Prototyping China Factory · Rapid Prototyping China Parts Manufacturer
Standards referenced on this page
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ISO 9001 — Quality management systems — Requirements